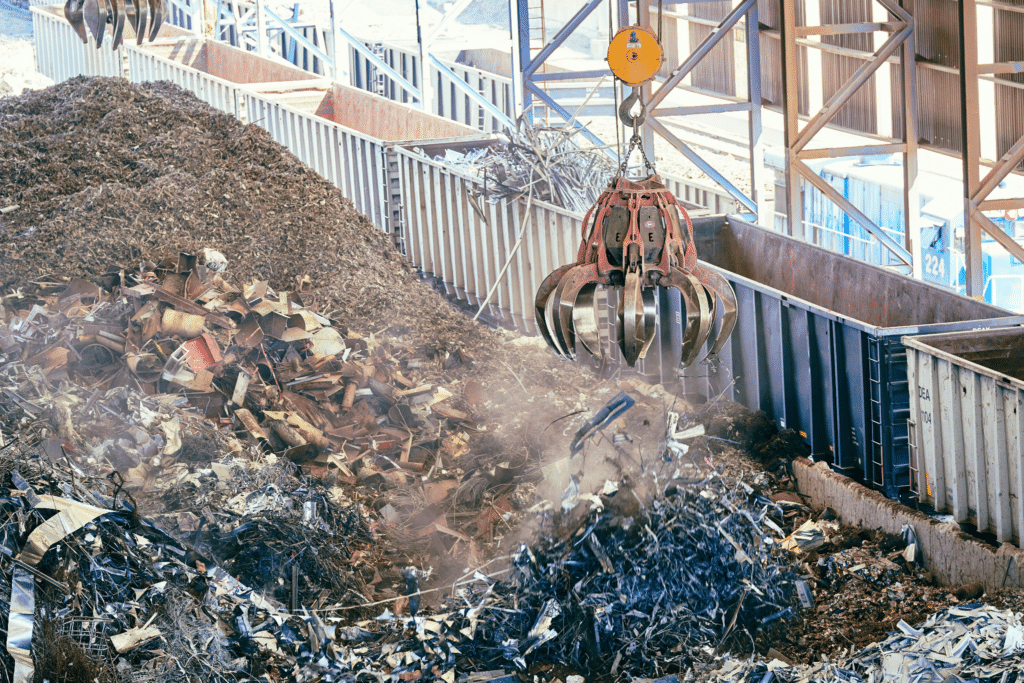
A scrap bin makes waste visible. A production line that runs differently from one shift to the next presents a less obvious problem, especially when finished output still meets the daily target. The rejected parts get counted, while the changing conditions behind them can escape the same scrutiny.
Manufacturing waste programmes often begin with losses that are easy to see and assign to a budget. That leaves a harder question: what connects recurring defects, repeat processing, and stock held against an unreliable production run? As manufacturers examine resource use alongside production costs, the distinction between recording a loss and understanding why it keeps returning deserves closer attention.
The Short Answer: Variation Is Where Waste Starts
Process variation is one upstream cause of manufacturing waste. Rather than another waste category, it can create defects, overproduction, and excess inventory.
Lean distinguishes value-adding vs non-value-adding activities: waste consumes resources without adding customer value. Associated with the Toyota Production System and Taiichi Ohno, the seven wastes of manufacturing are overproduction, waiting, transport, over processing, inventory, motion, and defects; the 8 wastes of lean add non-utilised talent.
The aim of producing only what is needed becomes harder when usable output remains unpredictable.
The three Ms distinguish Muda, the waste itself, from Muri, or overburden, and Mura, or unevenness. Mura involves an uneven work pace, with alternating periods of rushing and waiting that create downstream waste. Its costs rarely appear under a heading called “variation.”
How Inconsistent Processes Feed the Classic Wastes
A process can hit its target on average while swinging far enough around it to produce parts outside specification.
Defects, Rework and Rejected Components
Consider an oven whose temperature drifts between production runs. If parts require a defined temperature range, excursions can leave components needing rework or rejection. An acceptable average temperature doesn’t rescue a batch processed outside that range.
Rework sends parts through equipment again, consuming additional labour and machine time. Rejected components become scrap when no approved recovery route exists.
Planners might then schedule extra units to cover uncertain yield, creating overproduction and excess inventory. In contrast, reducing waste through small batches limits exposure, but smaller batches alone don’t correct the drifting oven.
The Hidden Material and Energy Bill
The rejected component contains more than its raw material. Its production has already consumed heating energy and, where the process uses them, compressed air, coolant, and other resources. Scrapping it discards that production effort too.
Rework adds another resource bill. Repeating a heating cycle consumes energy again; adding unnecessary processing time to compensate for uncertain conditions creates over processing rather than control.
Industrial solid waste describes the physical discard, whereas lean’s seven wastes describe production losses more broadly. That distinction matters for sustainability: a waste-disposal record captures the rejected material, but not necessarily the resources spent making and replacing it.

Using Production Data to Catch Variation Early
Variation can’t be eliminated entirely. The practical task is distinguishing an expected spread from evidence that the process has changed.
Telling Normal Noise From a Real Shift
Common-cause variation belongs to the process as it currently operates. When that process is stable, its spread is predictable within statistical limits. Reducing it requires changing the underlying process rather than repeatedly adjusting individual results.
Special-cause variation signals something different: an unusual event or change worth investigating. A sudden temperature jump, for instance, prompts a search for a changed condition, not an automatic reset.
The distinction prevents over-adjustment. Changing a setting after every ordinary fluctuation risks adding variation to a process that wasn’t shifting in the first place. Operators need an agreed response rule, not an instruction to chase every reading.
What Control Limits and SPC Reveal
Statistical Process Control plots production measurements in time order. Control limits come from the process data; specification limits describe the product’s requirements. They answer different questions: “Has the process changed?” and “Does this part meet requirements?”
A point beyond a control limit, or a recognised non-random pattern, prompts investigation. Such a signal can occur while measurements remain within specification, creating an opportunity to investigate before rejection occurs.
However, a stable chart doesn’t prove that output meets requirements. A consistently off-target process still needs improvement. Lean Six Sigma and Kaizen provide frameworks for acting on these findings rather than treating the chart as the improvement itself.
Putting a Number on It With First-Pass Yield
First-pass yield records the share of units accepted without rework. Final yield alone can hide repeat processing because a repaired component eventually counts as acceptable output.
Tracking first-pass yield alongside scrap rate exposes different losses: recoverable defects and rework versus material that leaves production permanently. The quality factor of Overall Equipment Effectiveness (OEE) adds context within equipment performance.
These measures aren’t substitutes for resource accounting. Connecting rejected and reworked quantities to material consumption, processing time, and energy records gives the loss a defensible cost.
Building In-House Capability to Control Variation
A control chart needs an owner who understands its signals and has authority to follow a defined response. Software alarms aren’t a substitute for deciding who investigates, what gets checked, and how findings reach the next shift.
Specialist SPC training therefore needs to cover more than plotting points. Teams need practice choosing suitable charts, establishing valid limits, recognising signals, and separating containment of suspect output from correction of the process.
Trustworthy measurement comes first. Measurement system analysis (MSA) examines whether differences come from the parts or the measurement process, and structured core tools training connects that work with SPC, failure mode and effects analysis (FMEA), control plans, and production part approval (PPAP).
Together, these tools link anticipated failures, monitoring arrangements, and evidence supporting production approval, including process capability. That connection gives each chart a purpose: FMEA identifies what could go wrong, while the control plan specifies what gets monitored and how production responds.
Once an investigation establishes a cause, prevention needs to survive normal shift changes. Standardized work records the agreed method, 5S makes workplace conditions easier to maintain, and Poka Yoke introduces mistake-proofing where practical.
These measures don’t replace Statistical Process Control; they support the conditions the chart is intended to monitor.
Why Controlling Variation Is a Sustainability Lever
Process variation is easy to overlook because its consequences appear in separate records: scrap, rework, extra production, and reserve stock. Treating those records independently can leave their shared cause untouched.
Stabilising a process addresses avoidable losses before more material and energy enter rejected or repeated work. That places variation control within lean manufacturing and sustainability together, rather than treating quality and environmental performance as unrelated concerns.
Not every waste comes from variation. Nevertheless, a manufacturer chasing the seven wastes individually risks treating symptoms, while one investigating inconsistent processes addresses a cause.